Case study · Compresseurs Entreprises Larry
Producing for an industrial equipment manufacturer
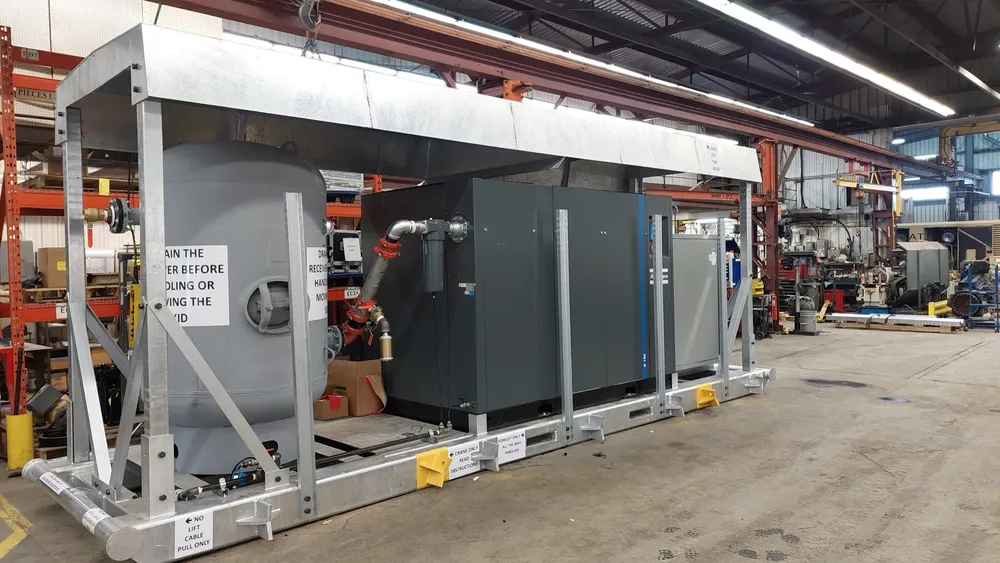
Compresseurs Entreprises Larry assembles industrial compressors. The metal chassis and mounts of every unit are produced with us, in lots.
- 4
- sub-assemblies per compressor
- 2
- weeks lead time per lot
- 0
- rework at assembly
The client’s problem
Each compressor needs an HSS chassis, a motor mount, a tank frame and brackets. Those parts went through a cutting shop, then a welding shop.
Saw-cut tubes needed grinding and a jig at assembly. The delay between the two shops pushed back the assembly line.
What he sent us
- 2D drawings of the four sub-assemblies, with overall dimensions.
- An existing chassis, to measure the real anchor points.
- The target assembly pace, in units per month.
What we changed in the design (DFM)
- Coped joints and notches moved to the laser cut: no more grinding, no complex jig.
- Motor mounting holes positioned by laser, removing secondary drilling.
- Two welded brackets merged into a single bent part.
- Critical tolerances identified with the client on the drawing, the rest left standard.
How we produced it
- 01
Prototype
A first complete chassis, measured on the critical dimensions, mounted on a real compressor at the client’s plant.
- 02
Program locked
Cutting program and welding fixture kept for every following lot.
- 03
Recurring lots
Laser cutting of the HSS, MIG welding in-house, coordinated powder coating, delivery by lot at the pace of assembly.
The result
The four sub-assemblies arrive finished, on a single purchase order, with a two-week lead time per lot. No rework at assembly since the approved prototype.
The client no longer coordinates two shops. He orders chassis and assembles compressors.